
Automotive
Industry 4.0 machine data collection from CNC machines and robots
Data collection from CNC machine tools and production line robots at the Hungarian plant of a Japanese automotive manufacturer: status, alarms, cycle times, tool and servo data in a time-series database, with per-machine Grafana views.
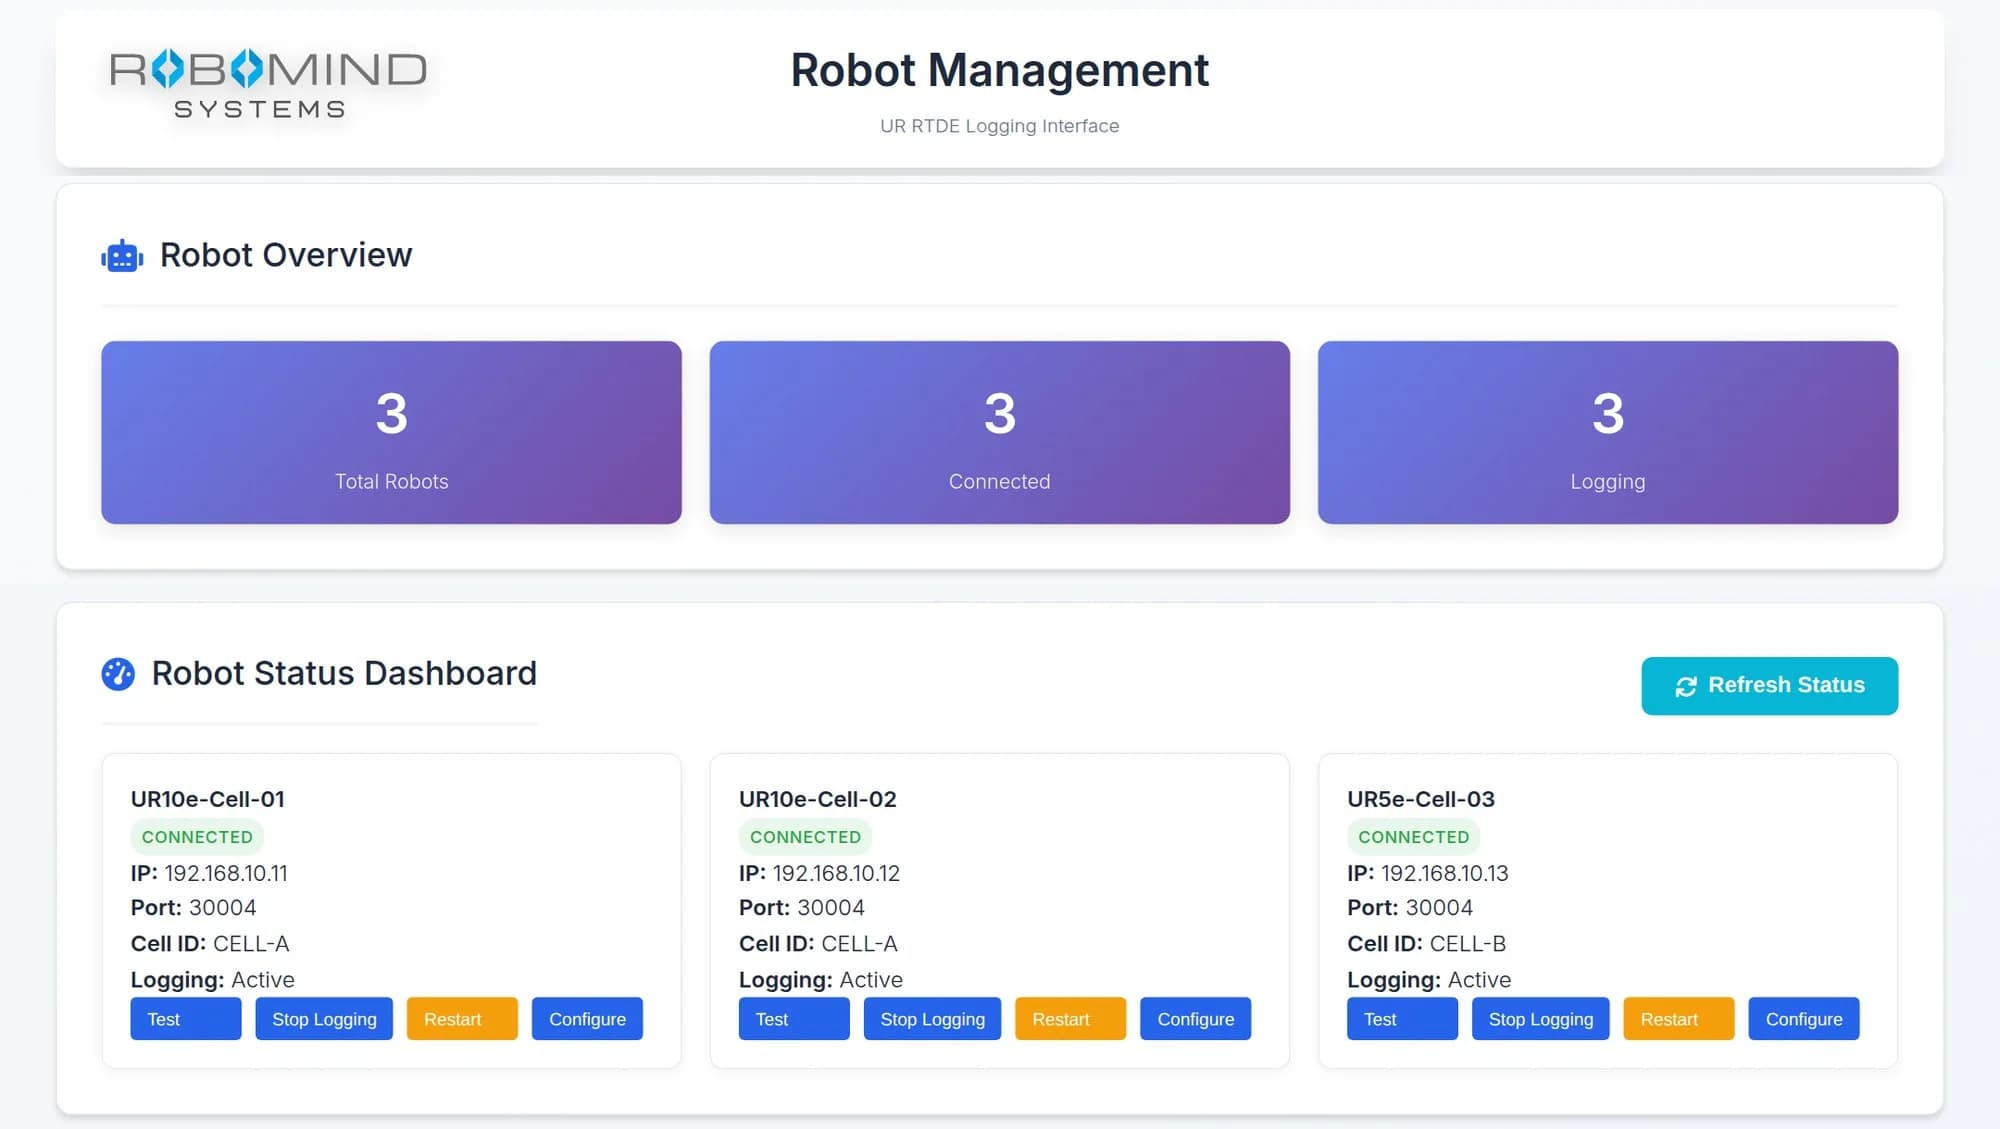
Task and implementation
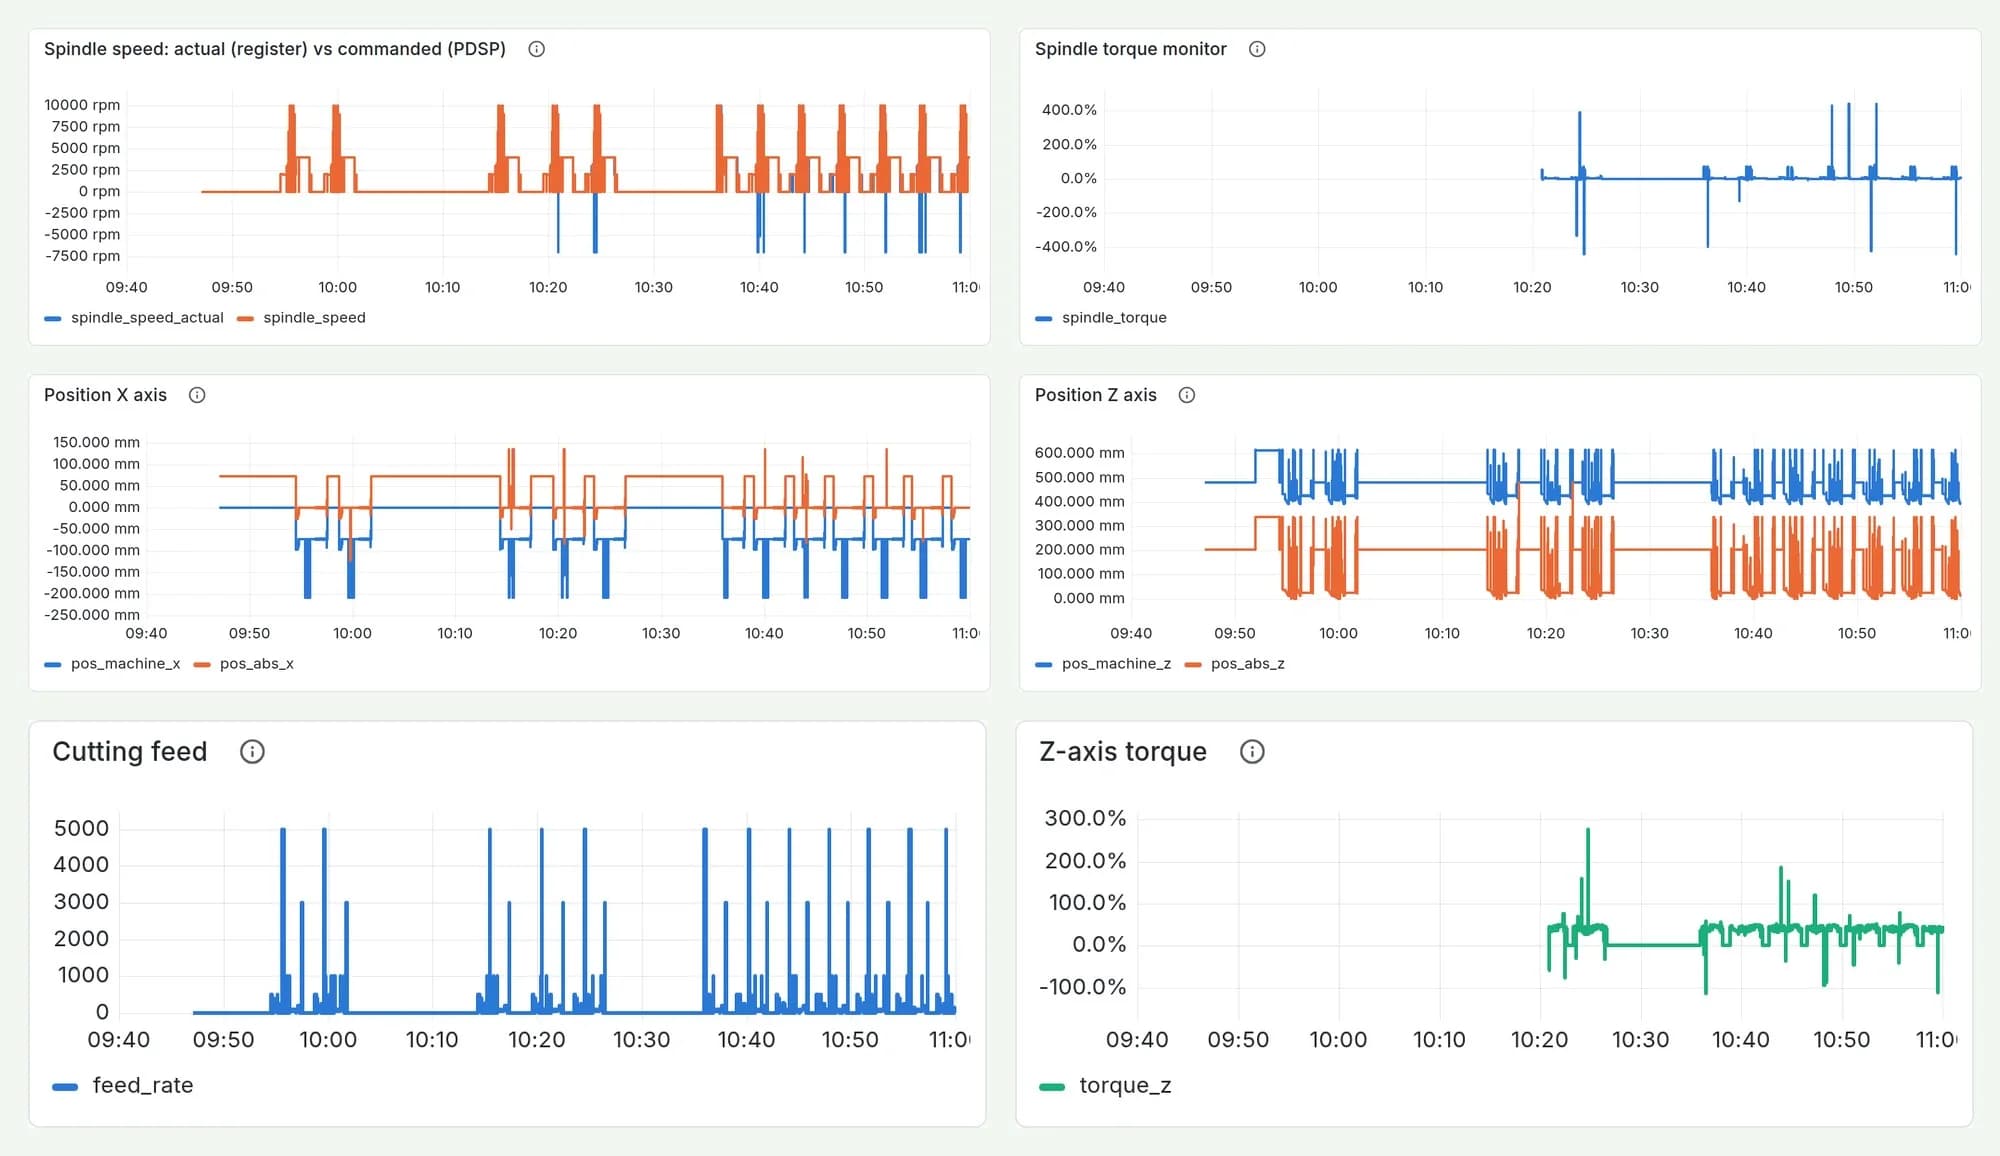
At the Hungarian plant of a Japanese automotive manufacturer, the status of the machining lines could previously only be seen on the machines' operator panels. The task is continuous data collection from 32 CNC machine tools – extended with condition diagnostics for further lines – so that utilisation, alarms and the condition of wearing parts can be analysed centrally, including retrospectively. Roll-out is phased: collection is already running on the first machine, and deployment across the entire machine fleet is in progress.
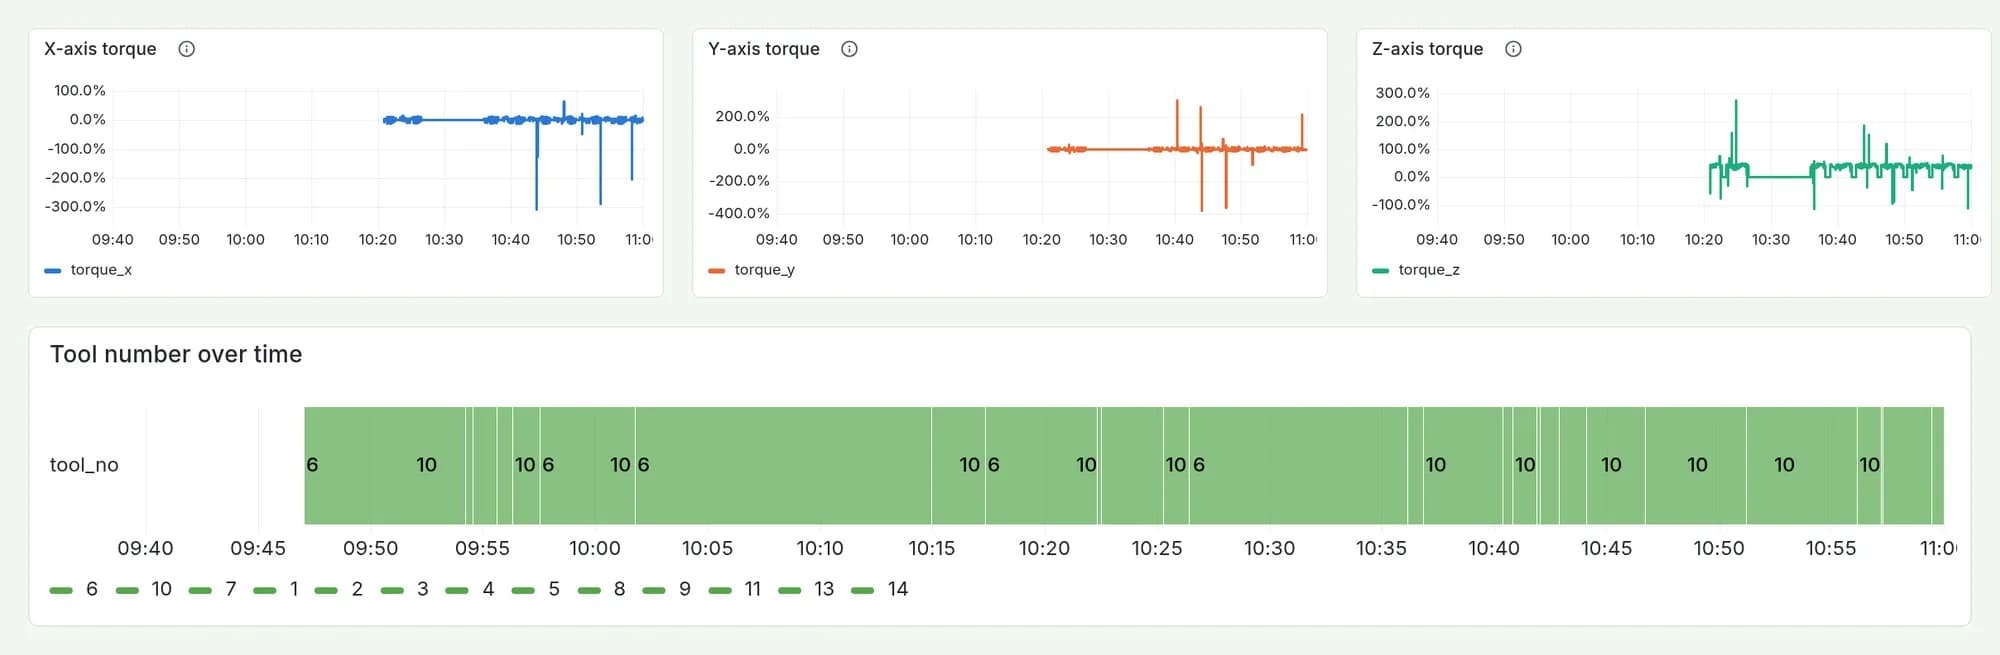
The collector developed by ROBOMIND Systems communicates directly with the CNC controllers and records, on change and with a regular heartbeat, the NC status, the alarms (decoded with the manufacturer's code table), the running program, cycle times and part counters, axis and spindle torque, servo load and temperature, and tool life and offsets. The data is stored in an InfluxDB 3 time-series database, and the per-machine Grafana view follows the customer's data point list.
An industrial edge PC runs in the cell with a segregated machine network and its own web-based configuration interface. Data from the Universal Robots arms on the production line is logged by industrial-PC gateways via the RTDE interface (joint positions, TCP forces, currents, temperatures, safety status), with complete separation of the robot and corporate networks. Data from OPC UA, Siemens S7 and Allen-Bradley PLCs as well as SMC air preparation units can also be connected to the same platform.
From data to decisions
The aim is to prevent unplanned downtime and to measure real utilisation: maintenance can be planned ahead from the alarm and load data, and cycle time deviations are immediately visible. The system can be built into machines made by Robot-Service as well as into an existing machine fleet.
Technology
- Direct CNC controller communication
- InfluxDB 3 time-series database
- Per-machine Grafana views
- Industrial edge PC with segregated machine network
- Universal Robots RTDE logging (industrial PC gateway)
- OPC UA, Siemens S7 and Allen-Bradley PLCs
- MQTT / MS SQL output
- E-mail alert on data loss
How a machine like this is built
From concept through FAT to final handover, every step happens in-house.
The full processRelated references
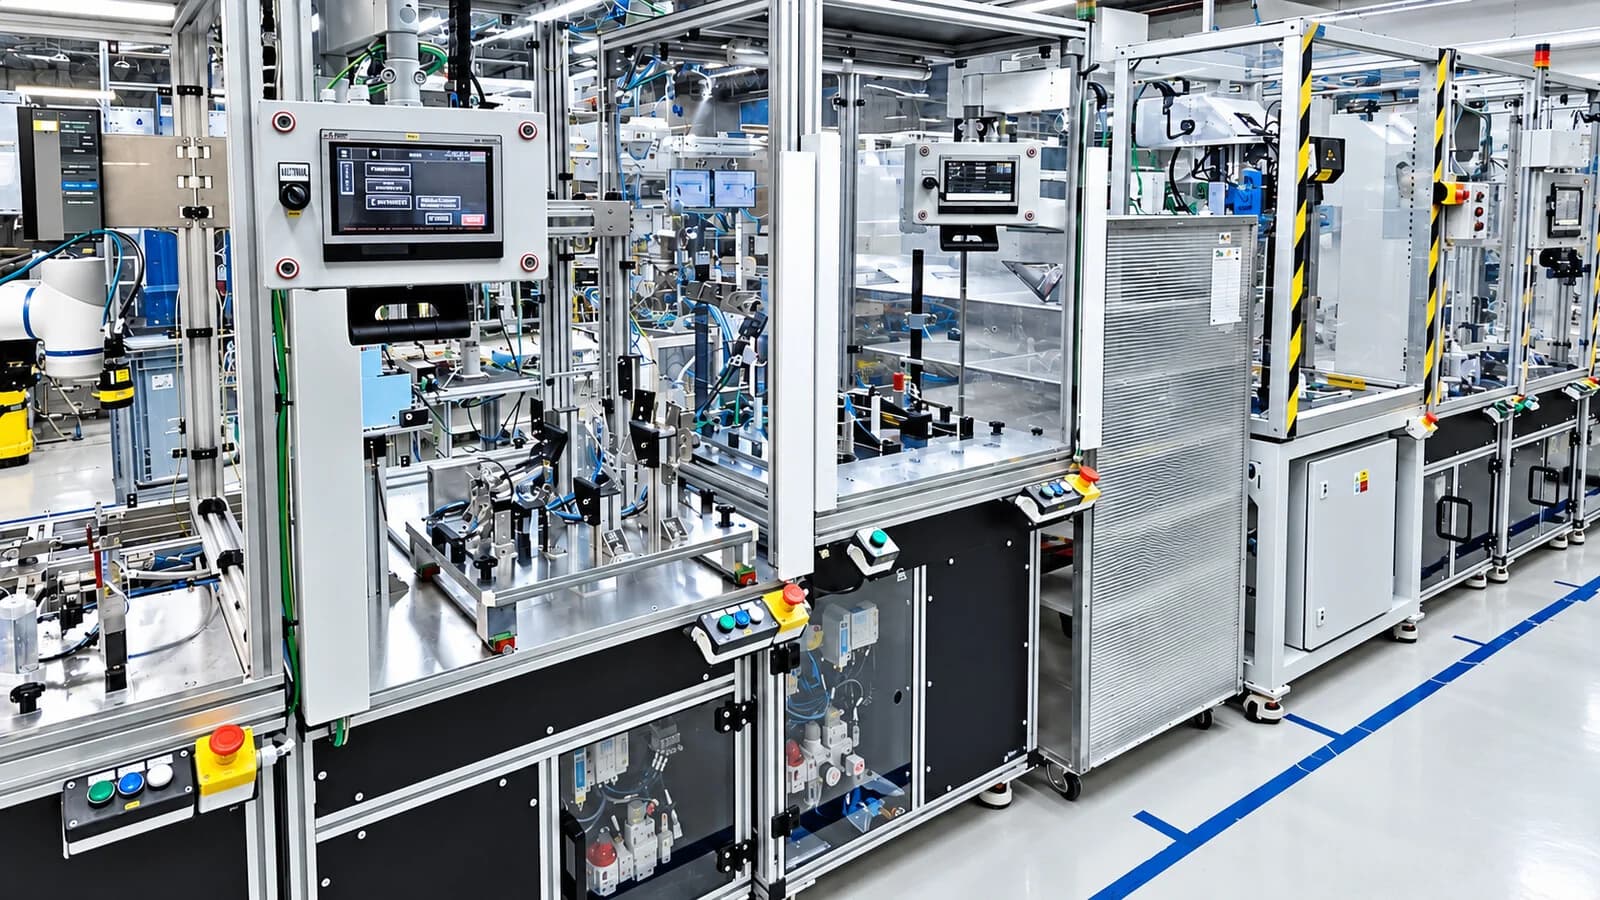 AutomotiveComplete automotive production linesTwo complete production lines with robotic assembly and MES connectivity. We were also involved in product development; 30 weeks passed from order to project completion with trial operation and final handover.View reference
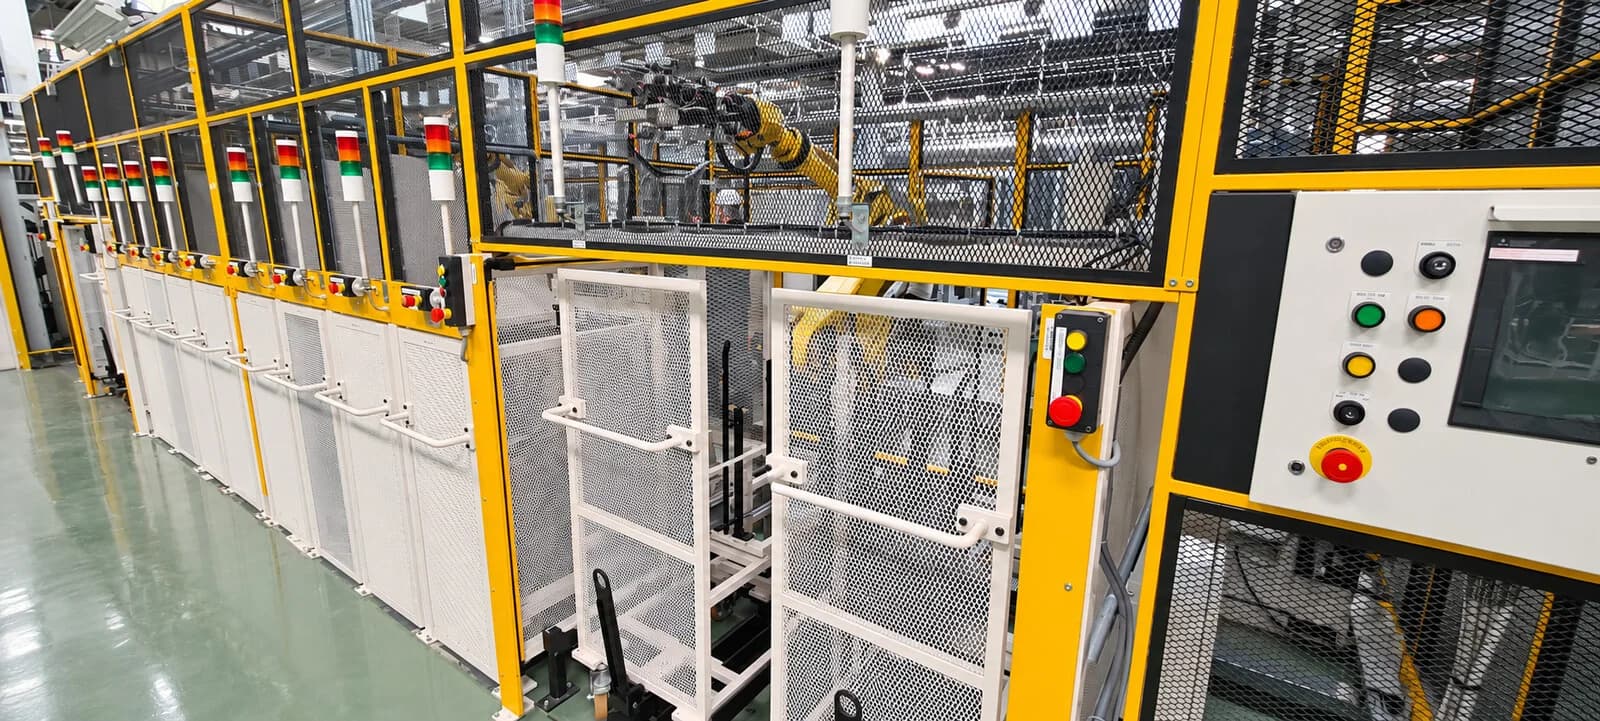 AutomotiveAutomated welding production line for an automotive plantA production line with two FANUC robots for resistance welding of nuts, bolts and threaded studs. Installation was scheduled to fit into the two weeks of the summer shutdown.View reference
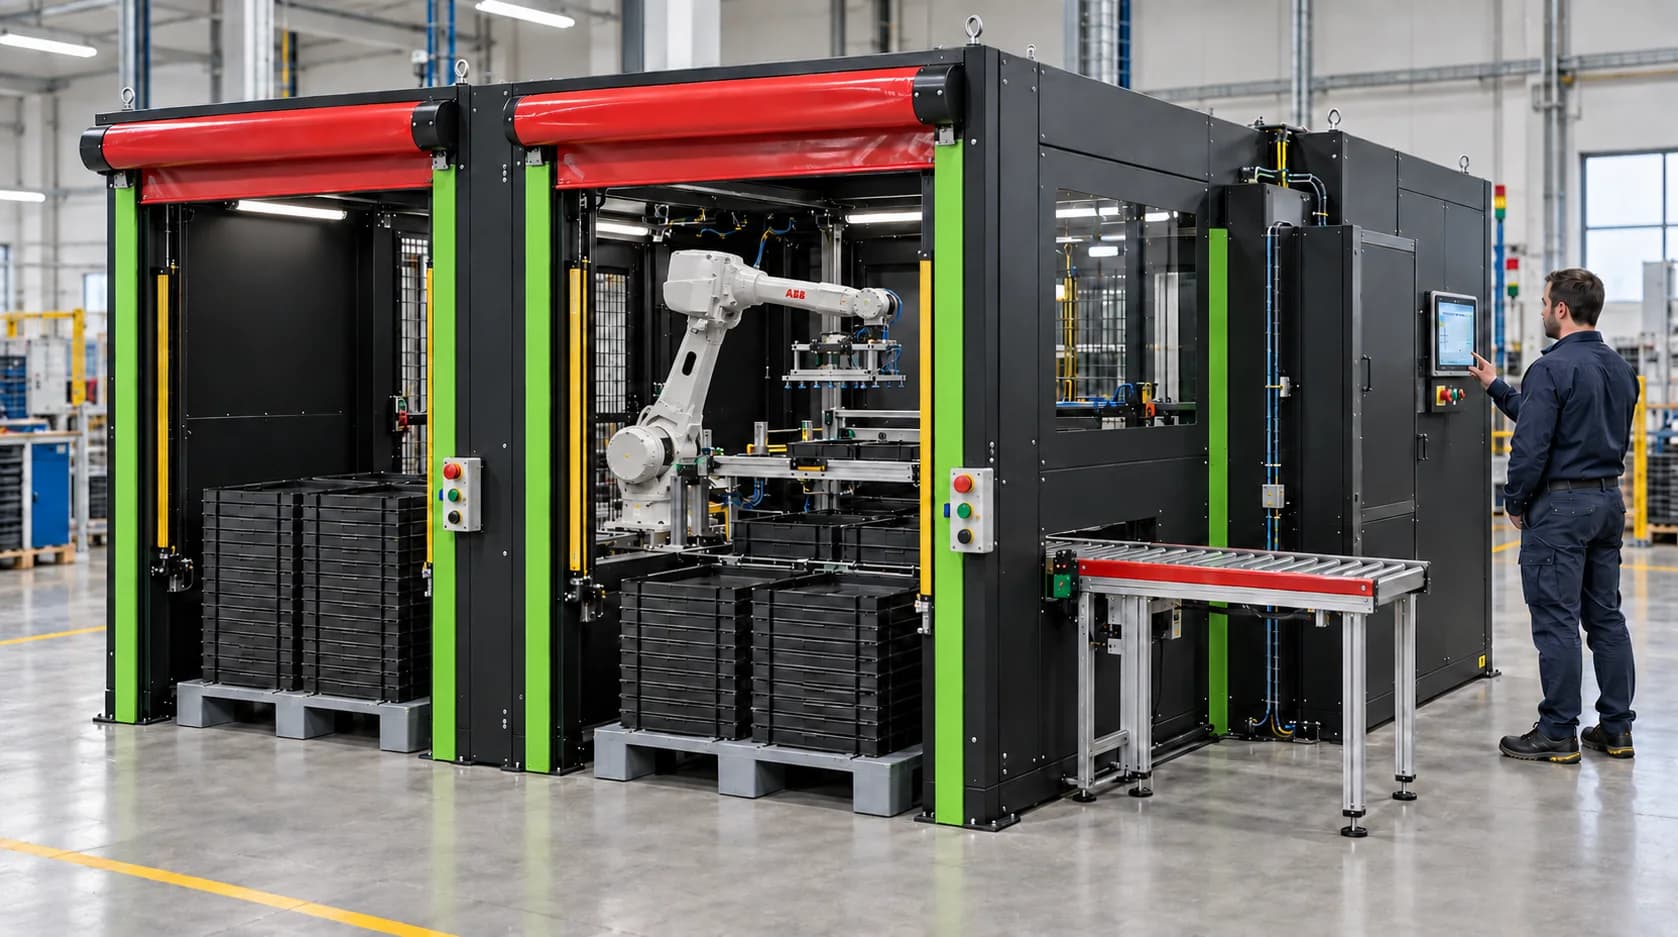 Electronics manufacturingESD-protected robotic packaging cellTwo ABB robots place electronic products from the workpiece-carrier conveyor into blisters. The cell handles defective parts separately and is prepared to receive automated material handling.View reference
Do you have a similar task?
Send us your specification or a short description of the task — our engineers will get back to you.